
Green means working condition
The sand is not oven-dried before pouring. “Green” describes the moist, workable condition of the mold material, not its color.
CASTING PROCESS GUIDE
Follow how prepared green sand forms the mold, how optional cores create internal geometry, and how pouring, cooling, shakeout and return sand reuse connect into one process.
01 / DEFINITION
Green sand casting uses a moist, clay-bonded sand system to form a mold around a reusable pattern. The sand is in a workable condition when the mold is poured, which is why the process is called “green” sand casting. After the metal solidifies, shakeout separates the casting from the mold and sends used sand back toward the preparation route.
The sand is not oven-dried before pouring. “Green” describes the moist, workable condition of the mold material, not its color.
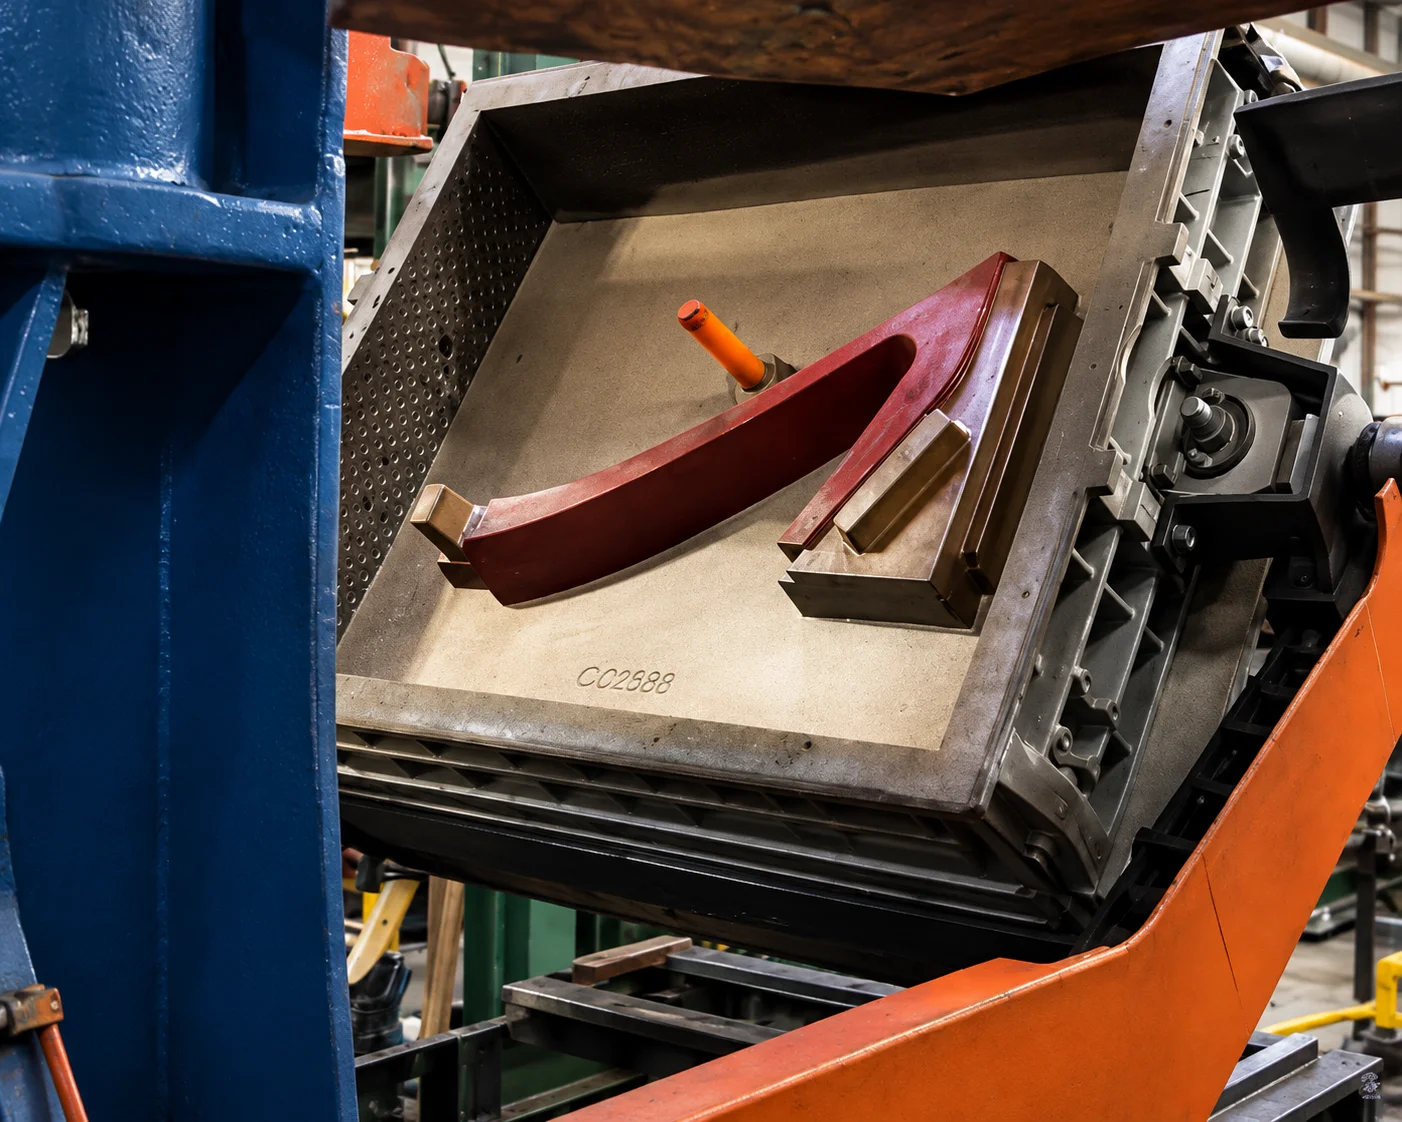
Prepared sand is compacted around a pattern. Once the pattern is removed, the cavity becomes the space that receives molten metal.
A core is introduced only when the casting design needs an internal passage, hollow area or feature that the pattern alone cannot form.
After solidification, shakeout separates the casting, flask and used sand so each material can move to its next process stage.
02 / MOLDING SAND
Green sand is a working material, not a single fixed ingredient. Its behavior comes from how the sand, binder, water and any process-specific additives are combined and conditioned.
Industrial sand provides the granular body of the molding material and the surface around which the mold is compacted.
Clay or bentonite helps the prepared sand hold together after mixing and compaction. The binder system is selected around the process.
Water activates the clay-based bonding behavior and influences how the sand flows, compacts and responds during molding.
Additives may be introduced according to the material, mold, surface and process requirements confirmed for the project.
WHY SAND CONSISTENCY MATTERS
Flowability decides how the sand reaches the available spaces around the pattern, compactability how it responds when it is compacted into the mold, mold strength whether the cavity survives handling, closing and pouring, and surface interaction how sand condition reaches the casting surface.
03 / PROCESS ROUTE
The route is shown as a process guide. The exact equipment, interfaces and enabled stages are confirmed around the casting and project requirements.
The pattern, parting arrangement and gating context are reviewed before prepared sand is introduced. Handling should leave clear access for molding, core placement and mold closing.
The pattern establishes the cavity, so its condition and parting influence how consistently the molding stage reproduces the intended geometry.
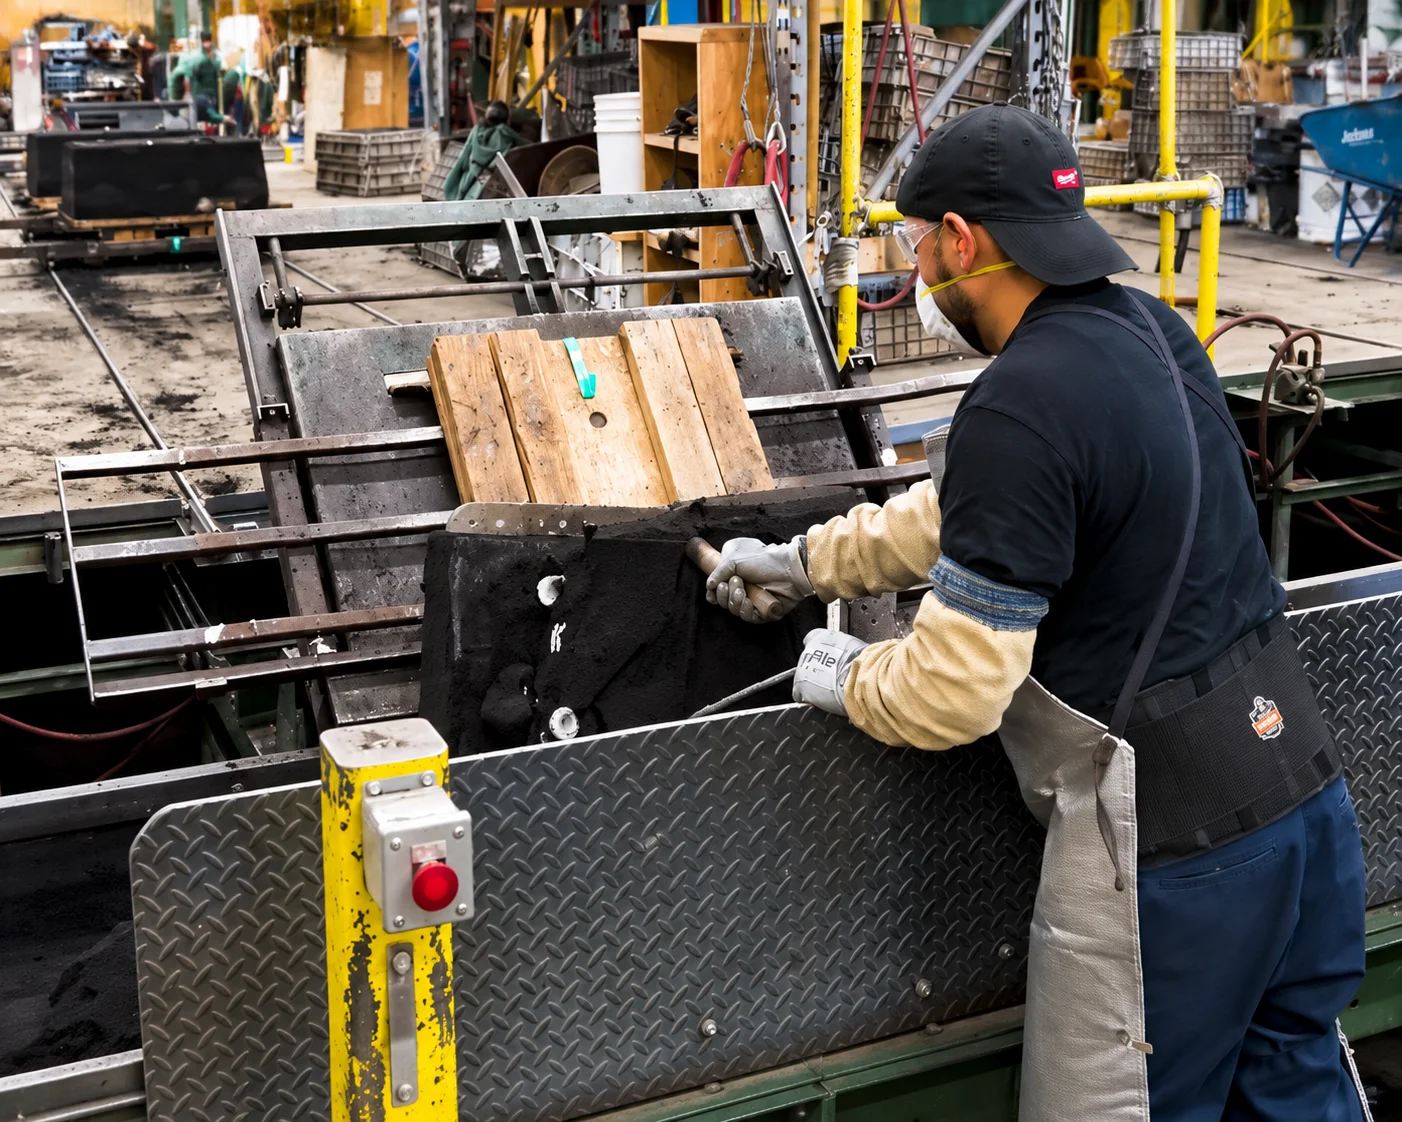
Return sand and new sand are received, screened or cooled where required, then combined with binder, water and additives and mixed to a workable condition before transfer to the molding area. Used sand from shakeout returns through this same route rather than ending with the casting.
Sand condition becomes mold behavior, so preparation, mixing and the return route are one connected loop rather than three separate steps.
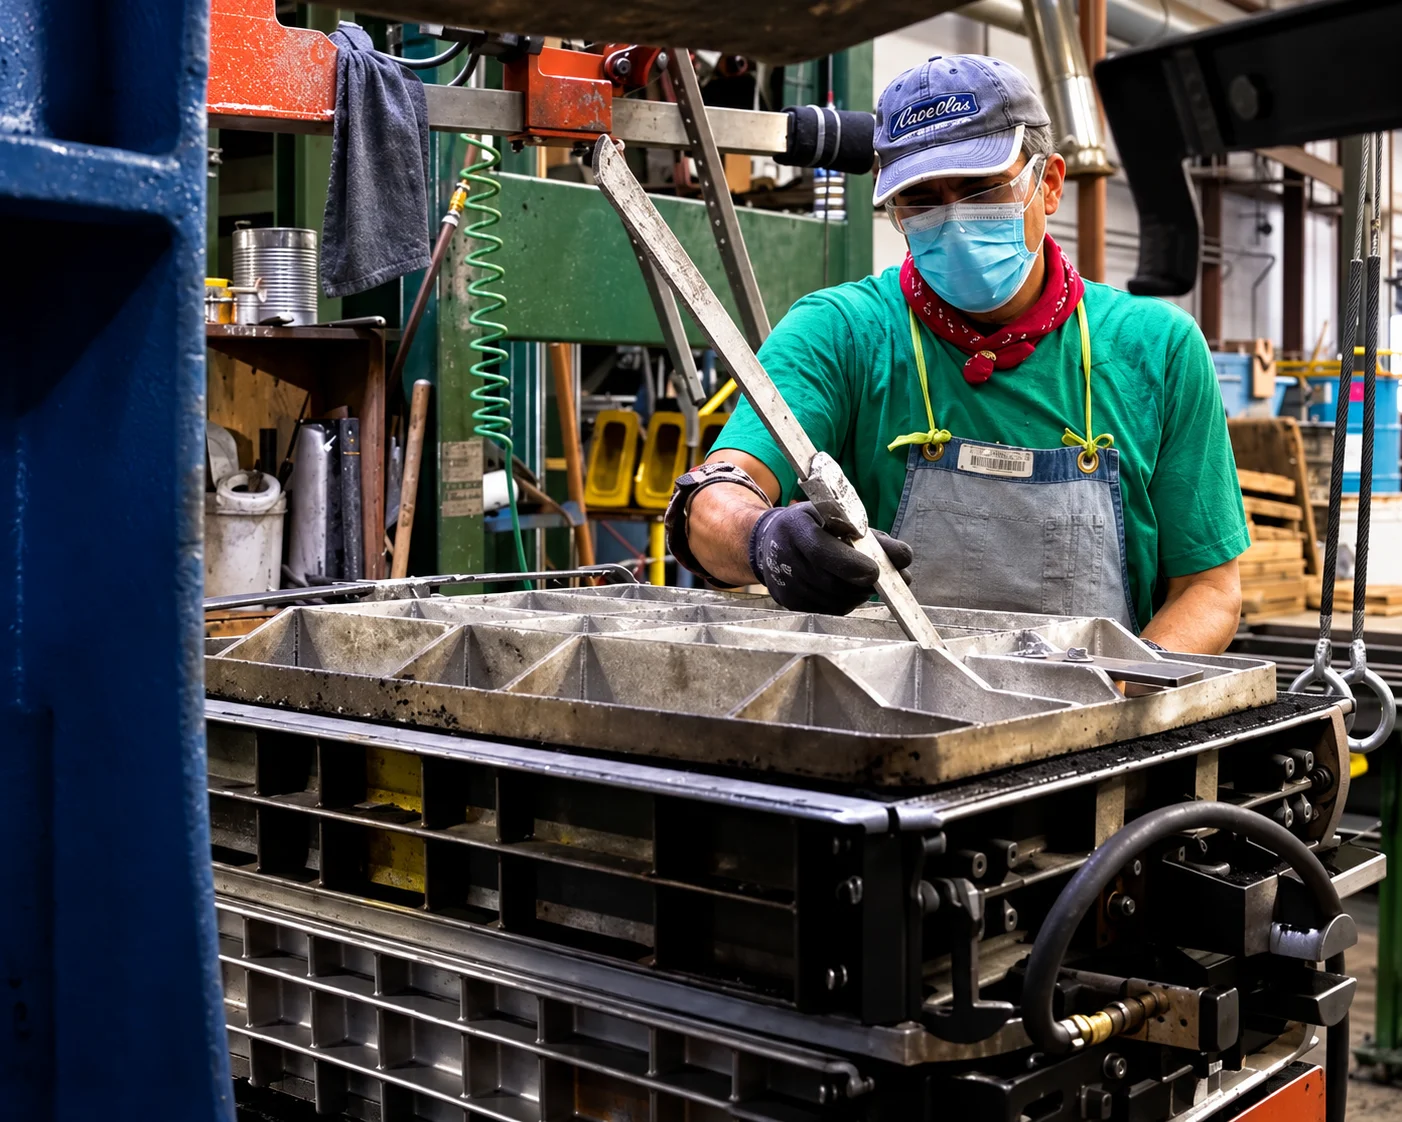
Prepared sand is filled and compacted around the pattern, and the pattern is withdrawn to leave the cavity. Where the design needs an internal passage or hollow feature, a core is made and set; the cope and drag are then aligned, the mold is closed and the gating path is checked before the metal handoff.
Cavity formation, core position and closing condition together decide whether the mold is ready to receive metal as intended.
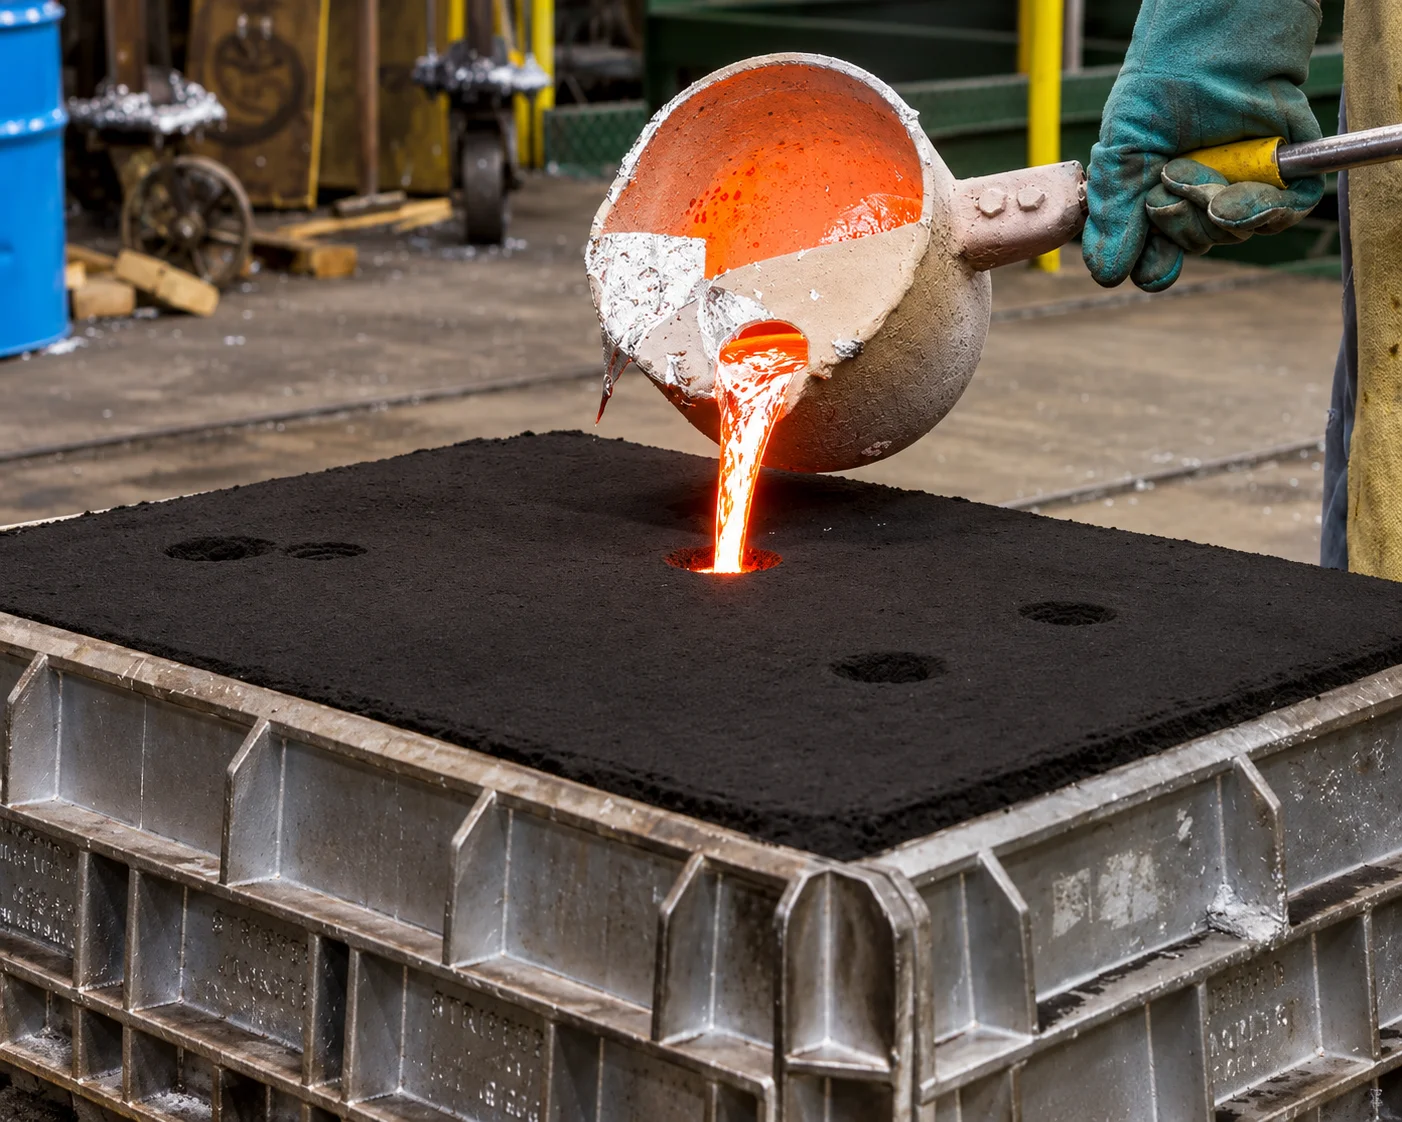
Metal is prepared in the selected melting system and transferred to the pouring position, with the mold, gating and pouring route treated as one handoff.
After pouring, the mold remains in or moves through the planned cooling path until the casting is ready, then shakeout separates the casting and flask components while used sand is collected for screening, cooling and conditioning.
The cooling route is project-specific and should not be reduced to a fixed time assumption; shakeout is where the casting route and the sand cycle divide.
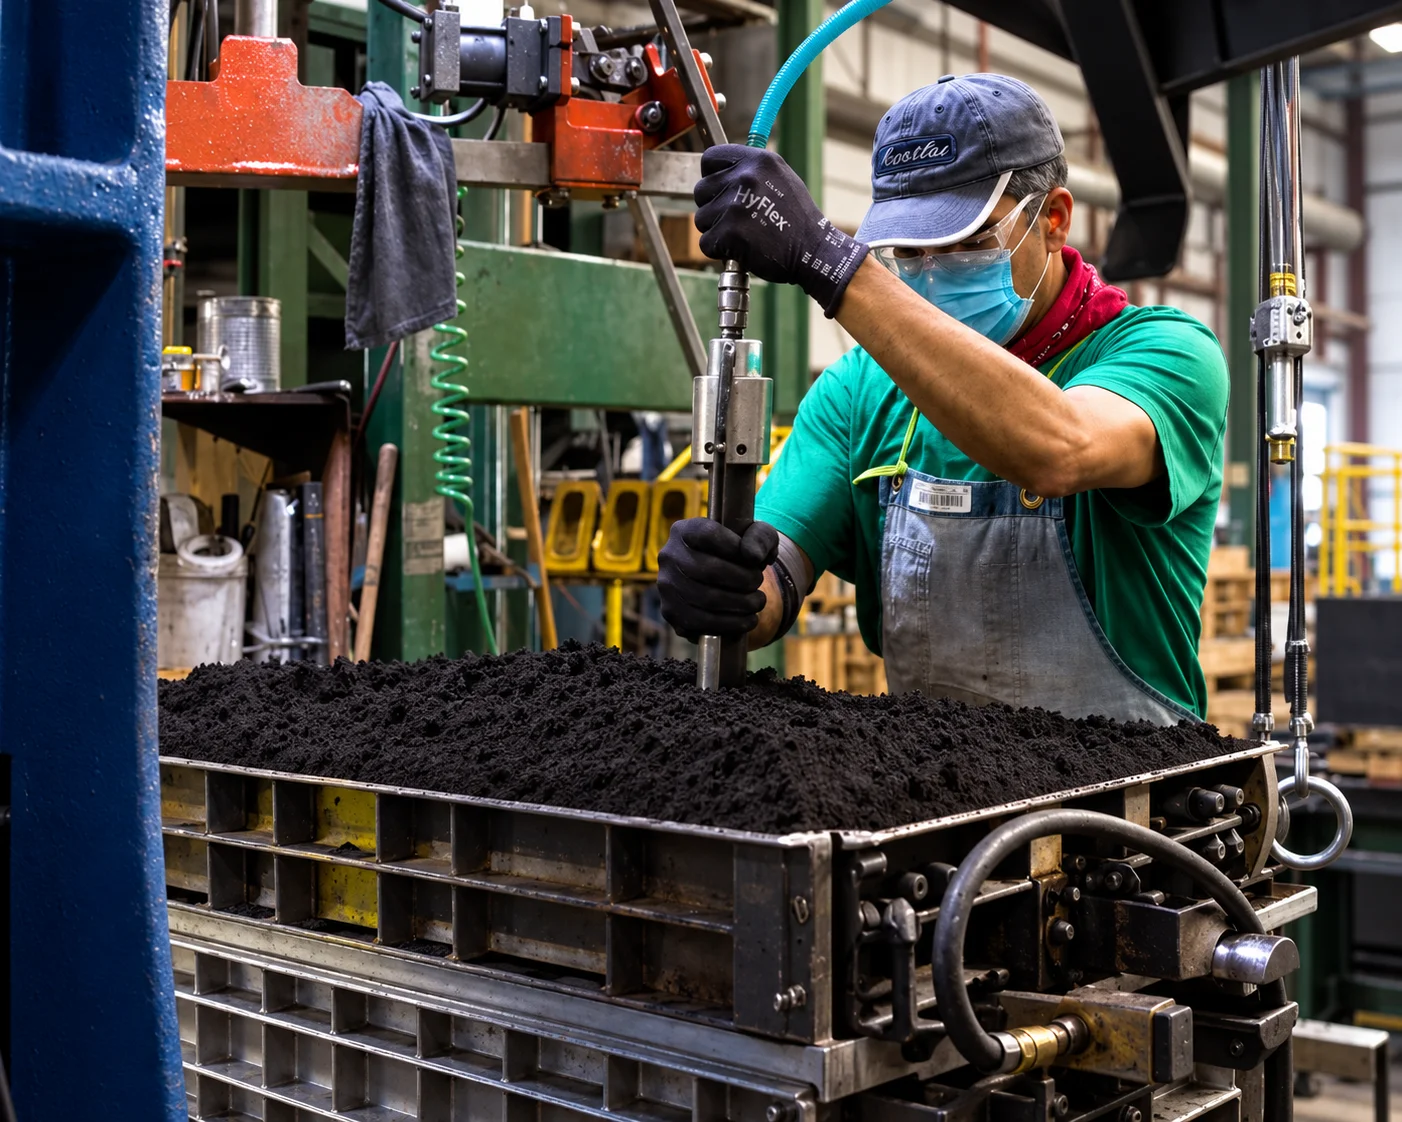
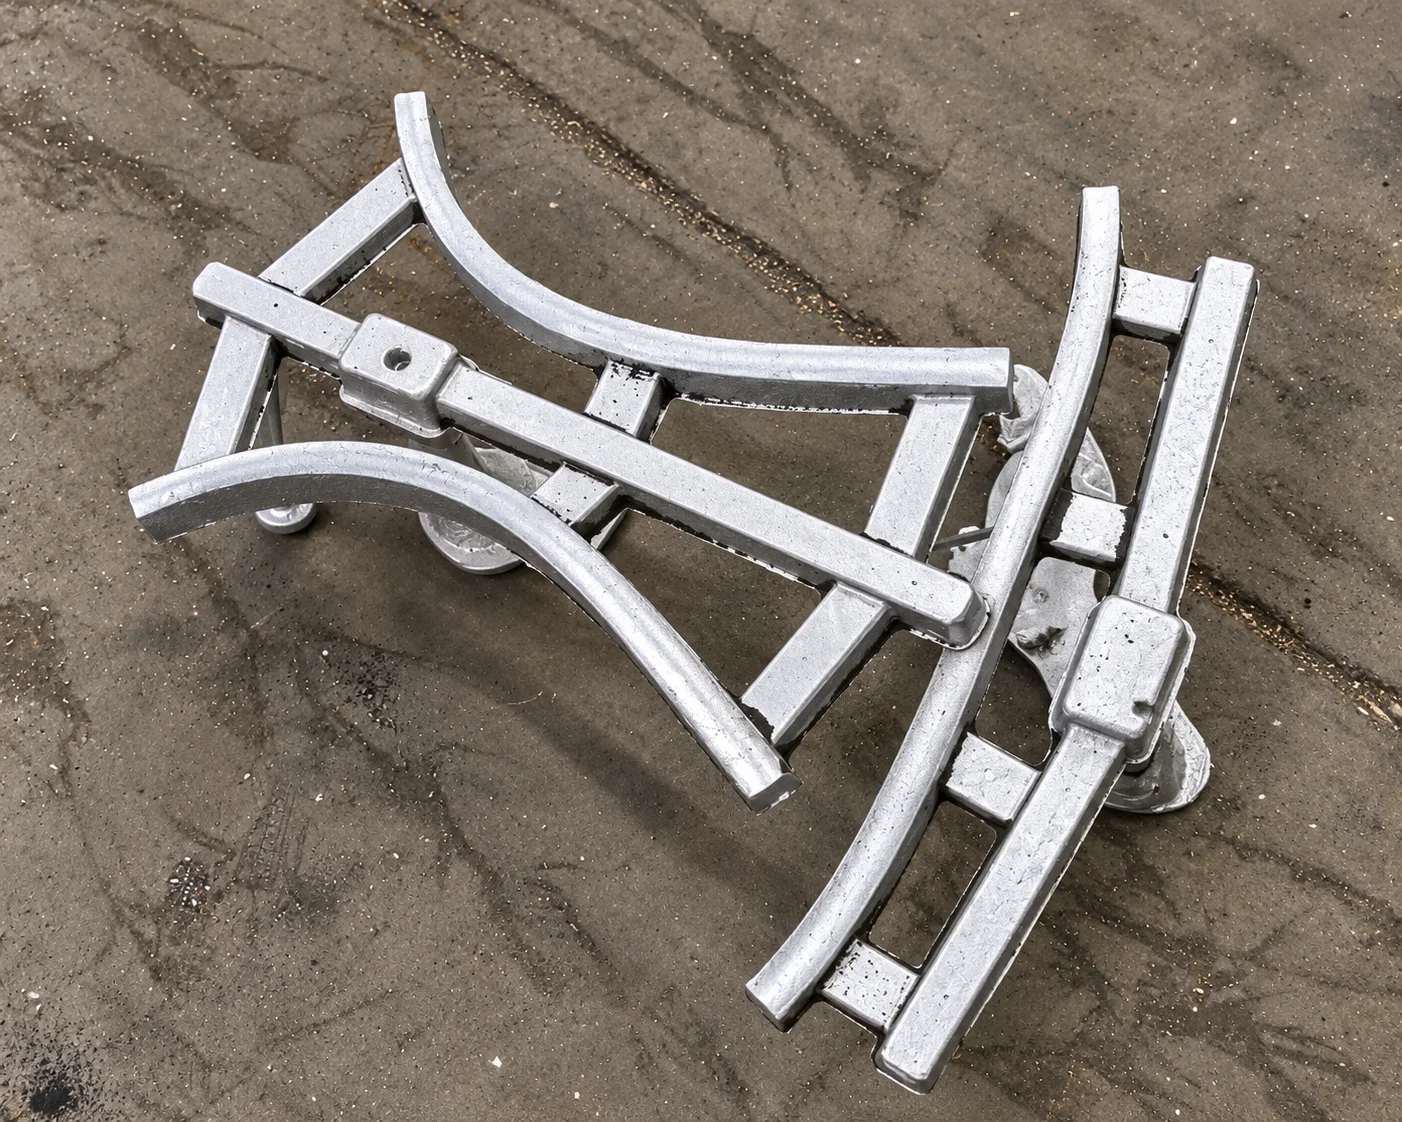
The separated casting moves through gate and riser removal, shot blasting, grinding, inspection or another finishing route defined for the part and project.
Only the finishing stages supported by the project scope are included, so the handoff to inspection, machining or shipment stays visible.
04 / SAND CYCLE
Return sand, cooling, dosing, mixing and testing are connected stages, not separate topics. Used sand from shakeout is screened, cooled, buffered and combined with new sand, binder, water and additives before it returns to molding as prepared sand. The objective is a repeatable working condition, not a universal recipe or a fixed limit.
After shakeout, the used sand route returns toward separation, cooling, conditioning and mixing rather than ending with the casting.
Screening, cooling, buffering and mixing describe the return route shown here. Any deeper reclamation, external disposal or additional treatment should be defined separately around the foundry’s sand condition and project scope.
05 / INVESTIGATION FRAME
The factors below are possible contributors, not absolute diagnoses. Review the related stage, available evidence and process condition before deciding on a correction. A deeper defect and remedy review belongs to the process discussion rather than this overview.
| Issue | Possible Contributing Factors | Related Stage |
|---|---|---|
| Sand Inclusion | Possible contributing factors may include sand condition, mold surface, handling or separation practice. | Sand Preparation / Molding / Shakeout |
| Gas-related Porosity | Possible contributing factors may include moisture, permeability, core condition, pouring or gas path. | Mixing / Core / Pouring |
| Mold Erosion | Possible contributing factors may include sand flow, mold strength, pouring interaction or mold handling. | Molding / Pouring |
| Misrun / Cold Shut | Possible contributing factors may include filling sequence, metal condition, gating or mold conditions. | Mold Making / Melting / Pouring |
| Mismatch / Dimensional Variation | Possible contributing factors may include pattern, cope / drag alignment, mold handling or cooling. | Pattern / Closing / Cooling |
06 / APPLICATION FIT
Green sand casting may suit several industrial casting families. Every entry below is a typical application, not a customer case or a guaranteed result.
Typical application for parts where mold route, material, output and downstream requirements are reviewed together.
Typical application for flow-related and housing castings where cavity, core and finishing needs should be considered.
Typical application for industrial components planned around geometry, material and production route.
Typical application for equipment castings where part range, mold handling and sand cycle need a connected review.
GREEN SAND CASTING VS SHELL MOULDING
| Dimension | Green Sand Casting | Shell Moulding |
|---|---|---|
| Mold Material System | Moist clay-bonded sand mold | Resin-coated sand shell mold |
| Pattern Condition | Reusable pattern route | Reusable pattern / tooling route for shell forming |
| Mold Form | Compacted sand around the pattern | Thin shell formed around the pattern |
| Sand System | Return sand conditioning and reuse are central to the route | Shell sand and shell handling follow a different process system |
| Key Process Focus | Sand preparation, molding, cores where required, pouring and return sand | Shell preparation, curing, pouring and shell handling |
| Main Equipment Focus | Sand plant, molding, optional core, melting, cooling, shakeout and cleaning | Shell moulding, core, melting, pouring and shell removal equipment |
07 / QUESTIONS
These are the questions that come up first when a green sand route is being weighed against no-bake, shell or investment casting, or when an existing sand system is being reworked. If yours is not here, send the drawing or specification and it is answered against the actual project.
The route is not tied to one volume band. Its economics come from a sand system that is prepared in-plant and a pattern that is used again for every mold, so the cost per casting falls as the same pattern runs more often, while the pattern and its plate are the main setup in either case. At low volume the question is whether building that tooling is justified for the part; at high volume the molding method and the level of automation on the line join the same discussion. Both are confirmed against the drawing, the material and the project.
The parting direction and how much core the mold has to carry decide it. A matchplate route forms the cope and the drag from one plate at a single station, while a vertically-parted flaskless machine holds the parting plane vertical and forms both halves in the same chamber. How the sand is introduced belongs to the same decision, because a deep pocket is harder to fill and squeeze evenly than a shallow one. The molding method, and the flask or box it needs, are confirmed against the drawing, the material and the project.
Compactability, moisture, permeability and strength are read together because they move together: compactability guides the water added at the muller, permeability decides how the mold vents the gas the pour produces, and strength decides whether the mold wall survives closing and pouring. There is no universal target that applies to every plant; the working window belongs to the sand system on site and is confirmed by testing the mix through the shift. A change of metal, geometry or new-sand share is reviewed against that window.
No. A core is used only where the casting needs an internal passage or a hollow form that the pattern and the two mold halves cannot make. The pattern carries the core prints that position the core, and the core is normally made longer than the cavity so it can be seated and supported outside the casting. A long core may need further support against the buoyancy of the pour, and the design has to allow the core to be removed afterwards, or the opening it leaves to be closed in finishing. Core design, the prints and the pattern are reviewed together, against the drawing and the material.
Not as a single figure for the whole part. Tolerance is quoted per dimension and per direction: a dimension that lies entirely inside one part of the mold can be held closer than a dimension that crosses the parting line, where closing and handling enter the result. Surface condition and the stock left for machining are set by the drawing and by the face being machined, so an as-cast surface does not by itself change the allowance a machined face still needs. Which dimensions carry the requirement is confirmed against the drawing, the material and the project.
The route is used across the range rather than for one metal family: it is the common molding method in iron and steel foundries and is also used for aluminium, copper, magnesium and nickel alloys. What bounds the choice is the mold itself, because a clay-bonded sand has a working temperature limit, and the part — very large sections, or geometry whose stability or parting arrangement the process cannot serve — is weighed against another route instead. The metal and the route are confirmed against the drawing, the part and the project.
Most of it returns. Used sand is separated from the casting and the flask components, screened and passed over magnetic separation to take out tramp metal, then cooled and mixed again with makeup clay, water and any additive the metal requires before it goes back to molding. New sand is added and a burnt and dusty fraction leaves the loop, so the material circulates rather than ending with the casting. How much leaves, and where it goes, is defined around the sand condition on site and the local rules that apply to it.
It starts from the stage that could have produced it, not from the name of the defect. In this route, gas in the mold is mostly steam from the water the sand carries, inclusions point at sand condition, mold surface and shakeout, and dimensional faults usually trace back to closing, alignment or cooling. Where and when the fault was first seen — at shakeout, after blasting, at machining or at final inspection — narrows the stages that can explain it. The investigation frame on this page groups each issue with the stages that can contribute to it, and the correction follows the process evidence rather than the appearance of the fault alone.
START A PROJECT
Share the casting type, material, part range, process stage, sand-system question or equipment need. The first discussion can focus on process fit before a line scope is defined.