
Wax defines the geometry
The wax pattern reproduces the part geometry that the ceramic shell and the metal will follow.
CASTING PROCESS GUIDE
Follow how wax patterns become a ceramic shell cavity, how the wax is removed, and how the shell is prepared, poured, finished and inspected.
01 / DEFINITION
Investment casting uses a wax pattern to reproduce the required part geometry. Multiple patterns are assembled as a wax tree, then surrounded by a ceramic shell built through repeated coating and drying cycles. Once the wax is removed, the shell retains a cavity. Molten metal is poured into that cavity; after solidification, the shell is removed and the individual castings continue to cut-off, finishing and inspection. “Investment casting” and “lost wax casting” describe the same core principle: wax defines the geometry, is removed from the shell, and leaves the cavity that metal later fills.
The wax pattern reproduces the part geometry that the ceramic shell and the metal will follow.
Ceramic coating, stucco and drying are repeated around the wax tree until the shell can hold the cavity.
The wax pattern is removed from the shell, so the space it leaves becomes the cavity that metal later fills.
Patterns are joined through gates to a central sprue, so one shell build and one pour can carry a set of castings.
02 / SHELL SYSTEM
Slurry creates the ceramic coating, stucco applies refractory material to the wet layer, and drying conditions the shell before the sequence continues. The shell is the mold: its build and condition decide what the cavity can hold.
Forms the ceramic coating around the wax tree.
Applies refractory particles to the wet shell layer.
Build the shell through recurring dip, stucco and drying cycles.
Supports consistent shell condition and safe handling between cycles.
The shell is built in recurring coating cycles rather than in one pass, and each cycle ends with the layer ready for the next one.
Dewaxing removes the main wax content and creates the cavity; firing and preheating prepare the shell for the selected pouring route. They belong to one thermal sequence, but each has a different purpose.
03 / PROCESS ROUTE
The route is shown as a process guide. Final process conditions, equipment interfaces and controls are set around the specific casting project.
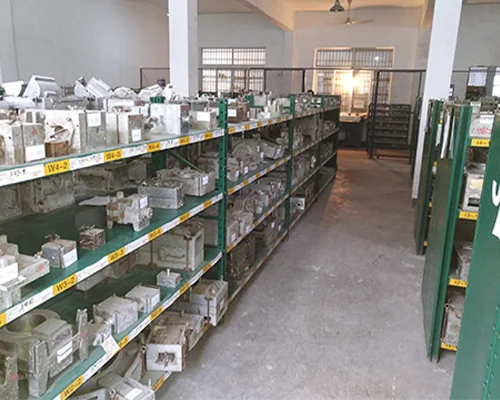
The die that forms the wax pattern is prepared before it is mounted for injection. Cavity and core details, the parting arrangement, ejection points and the surfaces that carry the part geometry are reviewed, so the pattern that comes out of it repeats from cycle to cycle.
The die is where the part geometry is fixed. The shell, the cavity and the final casting all reproduce what the die produces, so its condition and its record are settled before production rather than corrected during it.
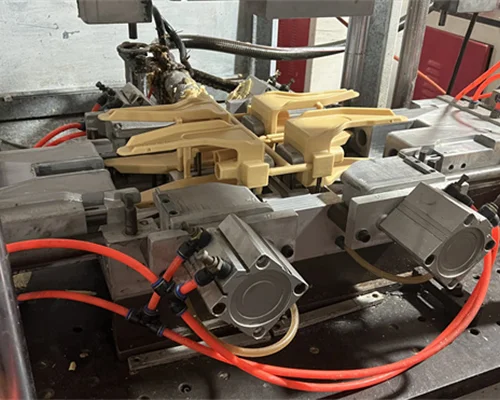
Wax is conditioned and injected into the closed die on an automatic injection machine. Injection pressure, dwell and the temperature of the wax and the die act together to fill the cavity and let the pattern solidify in the shape of the part.
Injection is the first place the part can go wrong without anyone seeing it: an incompletely filled or distorted pattern carries through the shell and only shows up much later. It is controlled as a machine cycle rather than as a manual operation.
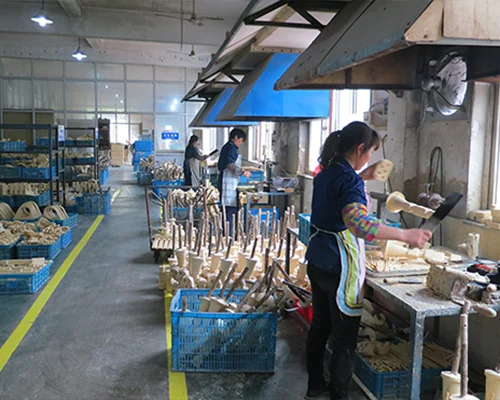
Individual wax patterns are joined — pattern to runner bar, and where the design needs it, smaller details welded onto a pattern — with a heated tool and assembly wax. Joint condition, alignment and support are checked as each pattern leaves the fixture.
The assembly becomes one wax body with the patterns, so a weak or misaligned joint is reproduced in the shell and then in the metal. Handling here decides whether the geometry survives to the pour.
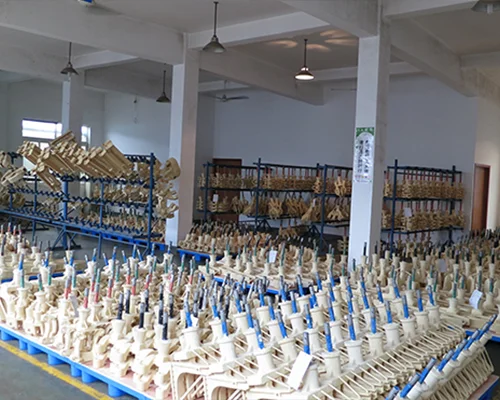
The prepared patterns are attached to a central sprue through gates, building the wax tree that will be coated and poured as one unit. The sprue carries both the mounting arrangement for the patterns and the flow path the metal will follow into each cavity.
The tree is what makes the route efficient, and it also fixes the feeding arrangement. Gate position, size and orientation decide how metal reaches the cavities and how the patterns are supported through shell building.
The wax tree is taken through repeated coating cycles on an automatic shell line: slurry dip, drain, stucco application and drying, layer after layer, until the ceramic shell has the build the route requires. The tree moves between stations as one unit.
The shell becomes the mold. Slurry condition, coverage and the drying between layers decide whether the shell can hold the cavity and survive dewaxing, firing and pouring.
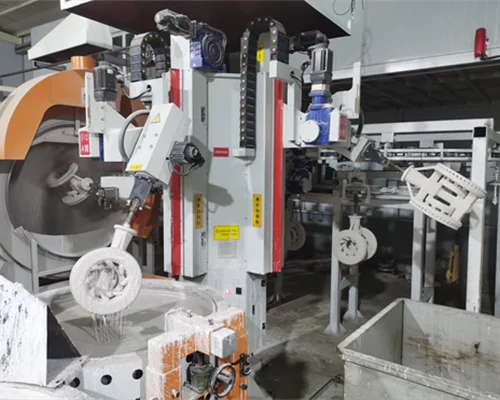
The coated tree enters the dewax operation, where the wax pattern material is removed from the shell. The wax leaves through the shell, and the space the pattern occupied becomes the cavity the metal will later fill.
Dewaxing is the point where the mold is created. Shell condition going in and the wax removal route going out both matter, and the stage is deliberately kept separate from firing and preheating.
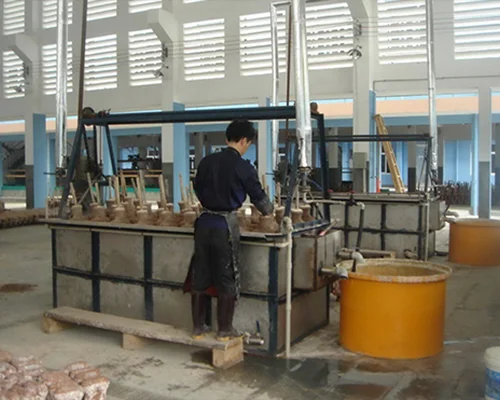
The dewaxed shell is fired and preheated in a furnace, which clears remaining pattern material from the cavity and brings the shell to the temperature the pouring route needs. Loading pattern and transfer are part of the same cycle.
Firing and preheating are a thermal stage with a different purpose from dewaxing: they prepare the shell, not the cavity shape. Shell condition after firing feeds directly into the pouring decision.
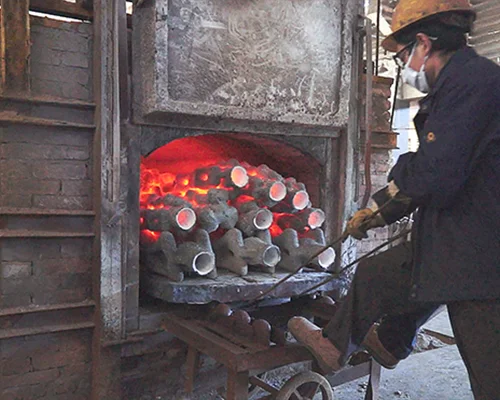
Metal is melted to the grade and condition the casting requires and poured into the preheated shell. Melting, transfer and pour are coordinated so the cavity is filled through the gating arrangement the tree provides.
Pouring is where metal, shell temperature, gating and handling meet. An incomplete fill or an inclusion introduced here is not recoverable downstream, so the sequence is controlled rather than left to the pour itself.
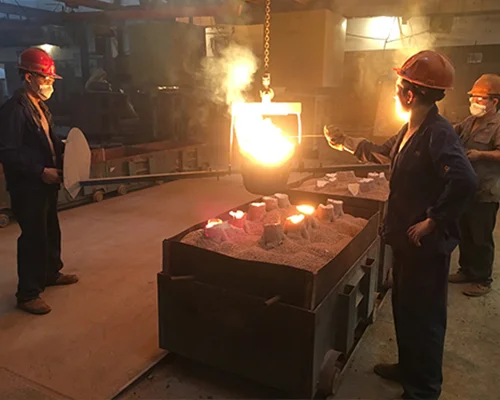
Where the drawing or the material specification calls for it, castings are heat treated — for example to relieve internal stress, to soften a casting for machining, or to bring the mechanical properties to the specified condition. The load, the cycle and the record of the batch belong to the same control scope.
Casting leaves a microstructure that is often coarse or uneven, so the required mechanical condition is reached by heat treatment rather than by pouring alone. Whether a casting is supplied as cast or heat treated follows the specification and the service conditions.
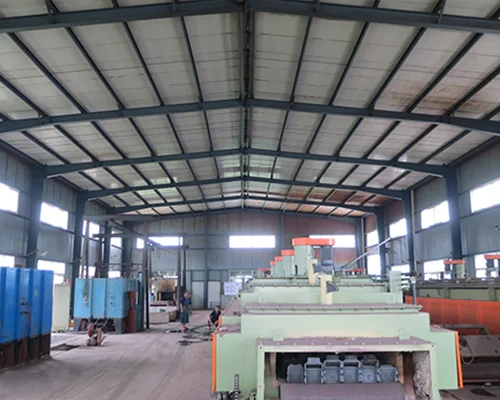
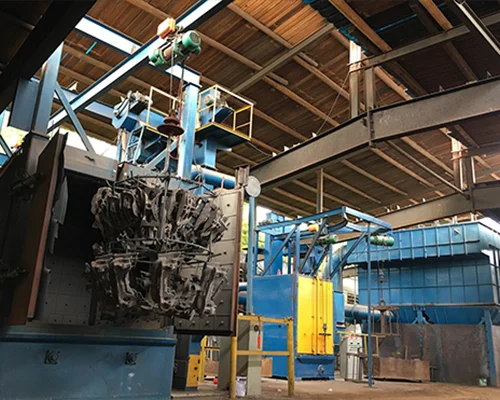
Once the shell has been removed and the castings are separated from the gating, they are shot blasted to clear residual ceramic, scale and surface material and to bring the surface to a consistent condition for inspection.
Blasting is what makes the surface readable. Residual shell or scale hides the casting condition underneath, so this stage is a checkpoint rather than only a cleaning step.
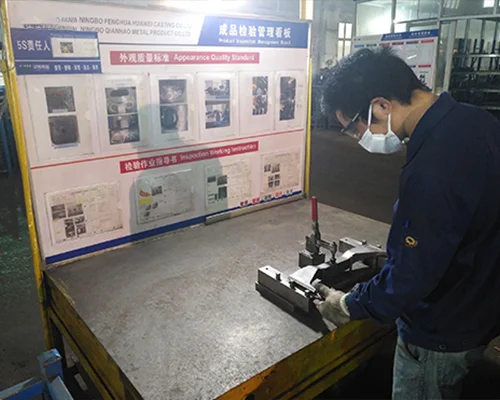
Castings are checked against the agreed requirements: the dimensions the drawing marks as critical, material verification, and whichever non-destructive or mechanical checks the project calls for. Results are recorded against the batch.
Inspection is what turns the process into evidence. Which checks apply is decided per part, so the inspection scope is agreed before production rather than added afterwards.
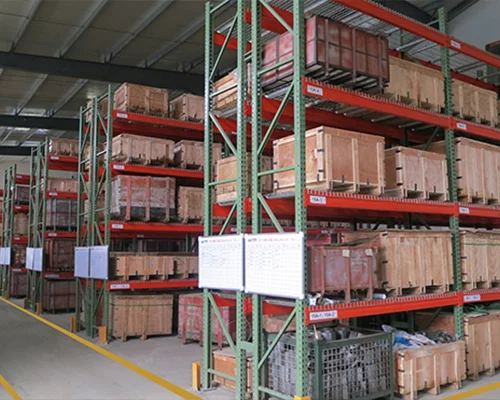
Accepted castings are marked, protected and stored before despatch, and the batch record travels with them. Whether a casting is packed as cast or after further processing follows the order.
The route ends at the customer rather than at the cleaning station. Handling and protection here decide whether the condition that was inspected is the condition that arrives.
04 / INVESTIGATION FRAME
The factors below are potential contributors, not absolute diagnoses. Review the related stage, available evidence and actual process conditions before deciding on a response. A deeper defect and remedy review belongs to the process discussion rather than this overview.
| Issue | Possible Contributing Factors | Related Stage |
|---|---|---|
| Wax Pattern Distortion | Wax condition, handling, cooling or assembly may be possible contributing factors. | Wax Pattern / Assembly |
| Shell Cracking | Shell build, drying condition, handling or thermal transitions may be possible contributing factors. | Shell Building / Drying / Thermal Stages |
| Inclusions | Material preparation, shell condition, pouring practice or cleaning may be possible contributing factors. | Shell / Pouring / Finishing |
| Misrun / Incomplete Filling | Mold condition, metal handling, pouring sequence or part geometry may be possible contributing factors. | Preheat / Pouring |
| Surface Defects | Wax pattern condition, shell build, metal interaction or finishing may be possible contributing factors. | Wax / Shell / Finishing |
| Porosity | Metal preparation, filling behavior, shell and process conditions may be possible contributing factors. | Pouring / Cooling |
| Dimensional Variation | Wax pattern, assembly, shell condition, thermal route or handling may be possible contributing factors. | Wax / Shell / Finishing |
05 / EQUIPMENT
Each category below is written out in full inside the stage it belongs to. This is a stage-oriented overview, not a catalogue: final equipment selection remains connected to the part, material, process route and project requirements.
Provides the die and the injection cycle that turn the part geometry into a wax pattern.
See the related stageJoins individual patterns and builds the tree that carries the metal flow path.
See the related stageRuns the repeated slurry, stucco and drying cycles that build the ceramic shell.
See the related stageRemoves the wax from the shell and fires it before pouring.
See the related stageMelts the specified grade and delivers it into the preheated shell.
See the related stageBrings the casting to its specified condition and prepares the surface for inspection.
See the related stage06 / APPLICATION FIT
Typical applications are a starting point for discussion, not customer cases or universal suitability claims.
Typical Application for complex, high-detail component geometry subject to project requirements.
Typical Application where shape, material and downstream condition need a clear review.
Typical Application for industrial components with process and material considerations.
Typical Application for flow-related parts where geometry and finishing can be evaluated together.
Typical Application for precision-oriented component needs; requirements should be reviewed case by case.
Typical Application for industrial components that may benefit from a wax-pattern and ceramic-shell route.
WHY CONSIDER INVESTMENT CASTING?
Complex geometry, Fine detail, Near-net-shape potential, Reduced machining potential and Material flexibility are the reasons a wax-pattern and ceramic-shell route is normally compared with other casting methods. Actual suitability depends on the drawing, material, required condition and production objective.
INVESTMENT CASTING VS OTHER PROCESSES
| Dimension | Investment Casting | Sand Casting | Lost Foam Casting | Die Casting |
|---|---|---|---|---|
| Pattern | Wax pattern tree | Reusable pattern route | Expendable foam pattern | Metal die / tooling route |
| Mold Type | Ceramic shell | Sand mold | Dry sand around coated pattern | Metal die |
| Pattern Expendability | Wax is removed | Pattern is reused in molding | Foam is replaced during pouring | Die is reused |
| Geometry | Complex detail can be reviewed | Depends on mold and core route | Depends on foam pattern and sand support | Depends on die, part and alloy route |
| Surface Capability | Discussed around wax and shell condition | Discussed around sand and finishing route | Discussed around coating, sand and finishing route | Discussed around die and process route |
| Production Considerations | Shell build and thermal sequence | Molding, cores and sand handling | Pattern, coating and sand reclamation | Die, machine and part requirements |
| Application Fit | Project-specific precision casting review | Project-specific casting review | Project-specific complex-casting review | Project-specific die-casting review |
07 / FAQ
These are the questions that come up when a part is being weighed against a wax-pattern and ceramic-shell route. If yours is not here, send the drawing or specification and it is answered against the actual project.
The route is chosen from the part rather than from a preference for a process. The wax pattern and ceramic shell earn their place where the drawing carries detail that a bonded sand mold would need several cores to reproduce, and where the part is small or medium rather than heavy. Where the casting is larger, the comparison moves to shell moulding or green sand, because the shell is a route for detailed parts rather than a route for heavy sections. Whether the volume justifies a wax die belongs to the same review, and a complete-line scope is defined only after the casting, material and production requirement are agreed.
It depends on what the tooling was built for. A wax pattern is injected into a temperature-controlled die that is arranged to release the pattern without damaging it, so tooling built for a room-temperature or sand-molding route is not a wax die. A pattern can sometimes be adapted, and how far that goes depends on its parting arrangement, its ejection details and the condition it is in. Send the tooling details with the drawing and it is answered in the technical review. Ownership and storage of any tooling are agreed with you before production starts.
Uniform wall thickness is the first thing reviewed, because a thin section and a thick section cool at different rates while the wax pattern, the ceramic shell and the solidifying metal each shrink differently. Draft is what lets the wax pattern leave the die and keeps the shell sound, so it is part of the drawing review rather than a detail added afterwards. Minimum wall thickness and corner radii are very dependent on the configuration and size of the part rather than fixed for the process, so they are confirmed against the drawing. Which faces stay as cast, and which are brought to their final dimension by machining, is settled on the same drawing with the tolerance class and the machining allowance for each part.
A tree is what makes the route economical, and it also fixes how the casting is fed. The sprue gives the shell build and the pour one unit to handle, so a single shell and a single pour carry a set of castings instead of one. The sprue is both the mounting surface the patterns are attached to and the flow path the metal follows, and the gates between the patterns and the sprue throttle where the metal enters each cavity. Gate and runner layout is therefore a tooling decision taken against the part, its material and its feeding requirements rather than a fixed pattern that every job follows.
The material is filtered by the service conditions first — wear, temperature, corrosion, pressure tightness — and then by whether a wax-pattern and ceramic-shell route can deliver the required properties. Steel and stainless grades, copper-based alloys and selected aluminium programs are the usual starting points, and the grade is confirmed in the technical review rather than selected from this page. Where the required condition of the metal cannot be reached by pouring alone, heat treatment belongs to the same discussion.
It follows the material specification and the service conditions rather than the process. Casting leaves a microstructure that is often coarse or uneven, so heat treatment is used to reach the condition the drawing asks for: relieving internal stress, softening a casting so that a machined face can be cut, or bringing the mechanical properties up to the specified grade. Whether a casting is supplied as cast or heat treated is settled in the technical review and written into the quotation, and heat treatment can be included with the casting when it forms part of the confirmed requirement.
No, and assuming one figure for the whole part is the most common source of disagreement. Tolerances are applied per dimension: linear tolerances for lengths, hole diameters and wall thickness, and geometric tolerances for contours, hole location and mating surfaces. A cored or curved hole may need a looser position tolerance than a straight drilled hole because of wax and shell behavior, while a critical face is normally brought to its final tolerance by machining rather than by the casting. Mark the dimensions that are critical and the surfaces that will be machined, and the tolerance class, the machining allowance and the finish are agreed per part before the die is cut.
It starts from the process stage that formed the feature, not from the defect name. The investigation frame on this page groups the characteristic faults of the route with the stage each one is usually traced back to, so the review moves through pattern and shell condition, the stage that produced it, and the pouring and finishing steps in order. A single cause is not assumed, because faults in this route often come from more than one stage at once. The starting point is confirmed against the drawing, the material and the project.
START A PROJECT
Share the casting type, material, part size, production requirement, current process and equipment need. The first discussion can focus on process fit before any line or equipment scope is defined.