
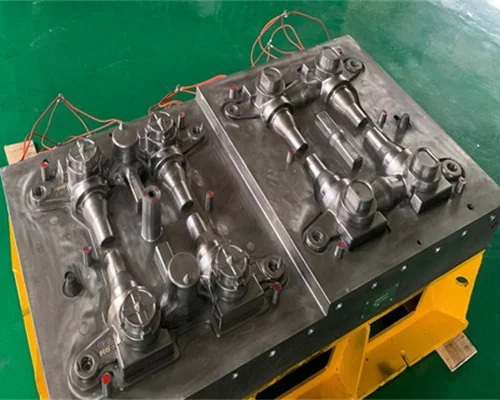
Heated metal pattern
A reusable metal pattern provides the heated surface around which the shell layer forms.
CASTING PROCESS GUIDE
Follow how a hot box core shooter and resin-coated sand form a thin shell, then move through mold closing, baking, pouring, cooling and shell removal.
01 / DEFINITION
Shell moulding uses a heated metal pattern and resin-coated sand to form a thin, bonded shell around the tooling surface. Loose sand is removed, the shell halves are closed into a mold, and the mold is baked before pouring. The mold is expendable, while the pattern is reused.
A reusable metal pattern provides the heated surface around which the shell layer forms.
Sand coated with resin contacts the heated pattern and bonds close to the tooling surface.
Sand that has not formed part of the shell is removed and routed away before closing and baking.
Shell halves are aligned and closed into one mold, which is then baked before pouring.
02 / SHELL SAND & HEAT
Shell moulding is built on a material interface rather than on a molding sand system: resin-coated sand meets a heated metal pattern, and the layer close to the tooling surface bonds. The route is planned for consistency, and no single fixed temperature or recipe is assumed here.
The sand carries the resin system that bonds the layer close to the heated tooling. Its condition, handling and distribution are reviewed together with the pattern and heating route rather than in isolation.
The heated metal pattern is the energy source for the bonding behaviour at the tooling surface. Consistency across the pattern matters more than any single assumed setting.
Only the sand close to the heated surface becomes part of the shell. The rest stays unbonded and is collected as a return material, so the shell and the loose sand follow different routes from the same contact step.
Coated sand is a prepared material: storage, transfer and condition decide whether it can be fed and distributed without interrupting the shell-forming cycle or damaging the tooling.
WHY THE HEAT INTERFACE MATTERS
Heat transfer decides where the bonding behaviour starts at the tooling surface, contact how much of the available pattern surface the coated sand reaches, shell formation whether the bonded layer keeps a usable cavity, and loose-sand removal what returns as material instead of becoming part of the mold.
03 / PROCESS ROUTE
The route is shown as a process guide. The equipment, interfaces and project-specific steps are confirmed around the casting and project requirements.
The metal pattern that defines the shell cavity is prepared before it enters the shooting cycle. Surface condition, parting arrangement, ejector references and handling points are reviewed so the shell can form on a surface that repeats from cycle to cycle.
In a hot box route the pattern is both the cavity reference and the heat source for bonding. Its condition carries directly into shooting, shell formation and closing.
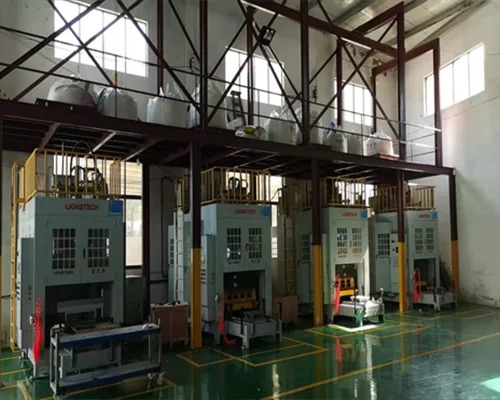
Shell halves and cores are produced on a fully automatic horizontal parting hot box core shooter. The machine carries clamping, heating, shooting and ejection as one cycle, so its station arrangement and cycle settings decide how shell production is paced.
The machine sets the repeatable cycle the rest of the route depends on: how the pattern is clamped, how sand is shot and how the finished shell is released.
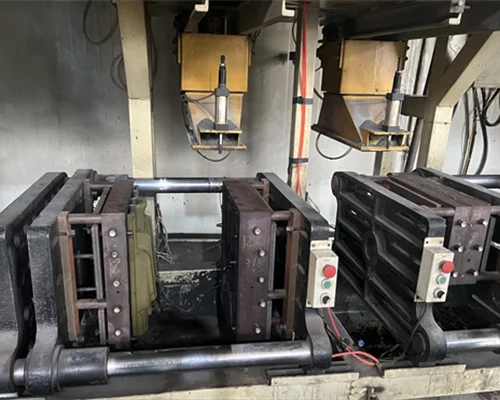
Resin-coated sand is shot into the closed pattern under the pressure and cycle defined for the tooling. The sand fills the cavity against the heated pattern surface, and the layer in contact with the tooling begins to bond.
Shooting decides whether the available pattern surface is reached evenly. Sand condition, pressure and venting act together, so an uneven shot shows up later as an uneven shell.
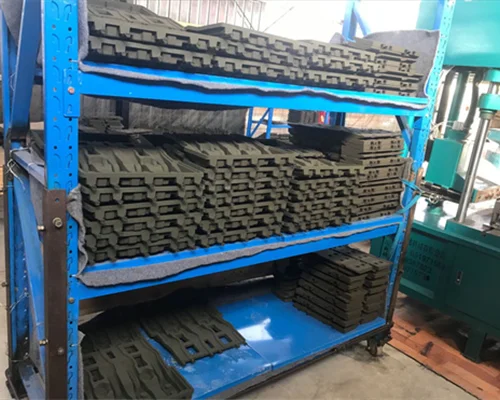
Only the sand held at the heated pattern surface bonds, so the result is a thin shell wall rather than a solid core. Unbonded sand is dumped or returned to the collection route before the shell is handled further.
The thin wall is the characteristic of this route: the minimum bonded sand forms the cavity surface while free sand follows a separate collection path. Wall condition should be checked before closing.
Shell halves are positioned against their alignment references and closed into a mold. The cavity, parting line and pouring access are checked at the closing station, and joining or clamping follows the method selected for the mold design.
Closing converts separate shell halves into the mold that will be poured. Alignment and joint condition decide cavity accuracy and mismatch risk.
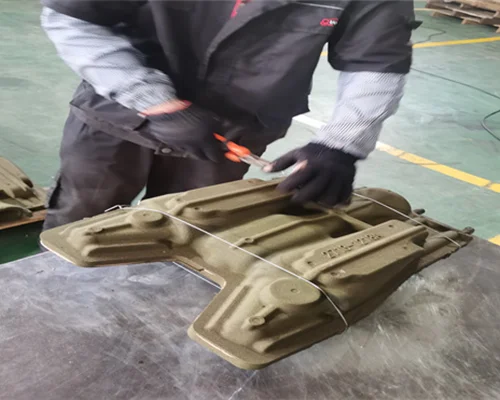
The closed shell mold is the unit that moves forward to baking and pouring. Its external condition, cavity access and stacking or handling arrangement are confirmed before it leaves the closing area.
Treating the closed mold as its own handoff separates shell production from the pouring route, so mold condition can still be checked while a correction is easy.
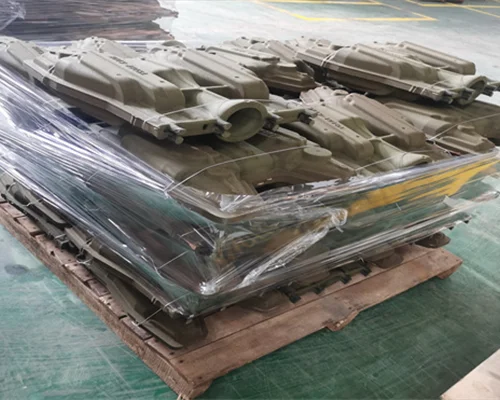
Closed shell molds are baked in the selected oven or baking arrangement so the bonded resin system reaches the condition the pouring route needs. Oven capacity, loading pattern and dwell are configured for the mold size and the production mix.
Baking completes the shell before it meets liquid metal. Mold condition after baking is part of the pouring decision, not a separate rework step.
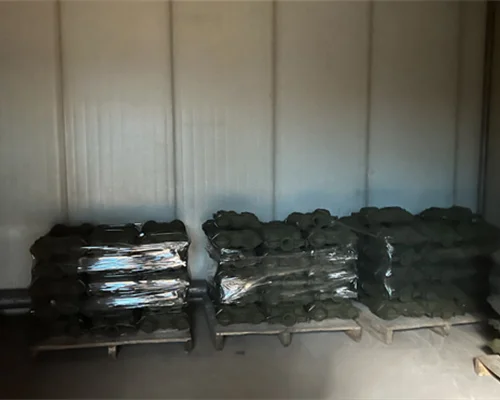
The baked shell mold enters the pouring line, is positioned for pouring and is filled through the defined gating arrangement. Melting, ladle handling, pouring sequence and mold movement are coordinated as one section.
Pouring is where the shell, gating, metal condition and handling meet. Coordinating the line keeps the pour sequence and the mold movement consistent.
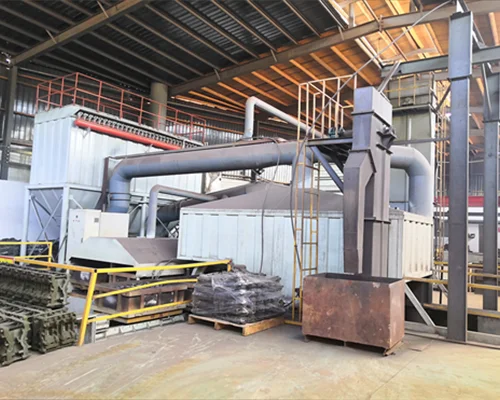
Poured molds move along the cooling route for the time the casting needs before the shell is removed. Cooling is handled on the line or in a defined holding area, and the transfer route to knock-out and finishing belongs to the same section.
Cooling sits between pouring and shell removal. Handling and floor space for the required cooling route should be planned with the line rather than added afterwards.
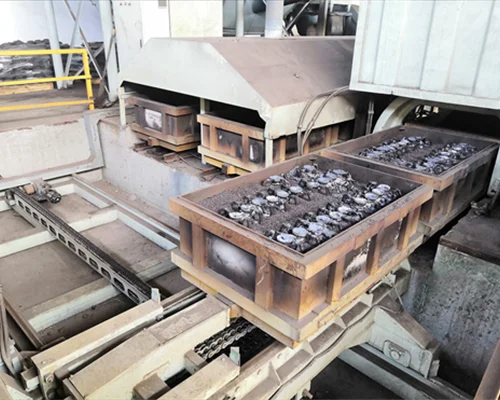
04 / SHELL CYCLE
Shell formation is the technical centre of this process: the heated pattern and the shot coated sand interact to create the mold surface while unbonded sand is removed. Closing and baking are related but distinct handoffs, and the cycle repeats for every shell half the mold needs.
The shot sand becomes a handled mold only after the unbonded sand is removed, the halves are closed and the mold is baked.
Core setting, mold backing or support, and whether baking is integrated into the cell or handled as a separate station, depend on the mold design and the pouring route. They are configured inside the nine stages above rather than presented as steps every project follows.
05 / INVESTIGATION FRAME
The factors below are possible contributors, not absolute diagnoses. Review the related stage, available evidence and actual process conditions before deciding on a response. A deeper defect and remedy review belongs to the process discussion rather than this overview.
| Issue | Possible Contributing Factors | Related Stage |
|---|---|---|
| Incomplete / Uneven Shell Formation | Possible contributing factors may include sand shooting, coated sand condition, venting or the pattern heating condition. | Sand Shooting / Thin-Wall Shell |
| Shell Cracking | Possible contributing factors may include the baking route, mold condition, handling or support during transfer. | Shell Baking / Mold Handling |
| Shell Breakage During Handling | Possible contributing factors may include shell wall condition, ejection, handling support or closing. | Thin-Wall Shell / Mold Closing |
| Mismatch at Mold Closing | Possible contributing factors may include alignment references, shell-half condition, joining or clamping. | Mold Closing |
| Sand / Inclusion-Related Surface Problems | Possible contributing factors may include loose-sand removal, shell surface condition, handling or the pouring interaction. | Thin-Wall Shell / Casting Line |
| Misrun / Cold Shut | Possible contributing factors may include pouring sequence, metal condition, gating, mold condition or handling on the casting line. | Casting Line / Cooling |
| Porosity | Possible contributing factors may include shell and mold condition, gas behaviour, metal condition or the pouring route. | Shell Mold / Casting Line |
| Dimensional Variation | Possible contributing factors may include pattern condition, closing alignment, baking, cooling or downstream handling. | Metal Pattern / Mold Closing / Cooling |
06 / EQUIPMENT
Each category below is written out in full inside the stage it belongs to. This overview is a process-oriented index, not a product catalogue: representative categories show where a technical discussion may begin without adding unverified specifications.
Provides the heated cavity reference that the shell is shot against.
See the related stageRuns the automatic clamping, heating, shooting and ejection cycle.
See the related stageStores, feeds and shoots resin-coated sand into the closed pattern.
See the related stageRemoves unbonded sand and carries the thin-wall shell forward.
See the related stageCloses shell halves into molds, bakes them and moves them on.
See the related stageConnects the baked shell mold to the casting line, cooling and shell removal.
See the related stage07 / APPLICATION FIT
These are typical application directions, not customer cases or guaranteed suitability. Review geometry, material, repetition, surface and downstream requirements together.
Typical applications where pattern condition, shell surface and dimensional requirements should be reviewed together.
Repeated components can be assessed against tooling, shell handling, pouring and downstream finishing needs.
Flow-related components may require a project review of geometry, shell assembly, cores and surface requirements.
Repeated production routes can be considered when the part, tooling, material and required controls are clearly defined.
SHELL MOULDING VS GREEN SAND CASTING
| Dimension | Shell Moulding | Green Sand Casting |
|---|---|---|
| Mold Material System | Resin-coated sand forms a bonded shell layer. | Moist clay-bonded sand is compacted into a mold. |
| Pattern Condition | A heated metal pattern is the reference the shell is shot against. | A reusable pattern defines the cavity during sand compaction. |
| Mold Form | Thin shell halves are shot, closed and baked into a mold. | Compacted sand forms the mold around the pattern. |
| Key Process | Sand shooting, thin-wall shell formation, mold closing, baking and pouring. | Sand preparation, molding, core setting, pouring and shakeout. |
| Sand System Focus | Coated sand shooting, loose-sand removal and defined handling. | Moist sand preparation, conditioning, return sand and reuse. |
| Main Equipment Focus | Hot box core shooting, coated-sand handling, closing, baking and pouring. | Sand preparation, molding, core making, mold handling and shakeout. |
08 / FAQ
These are the questions that come up first when a part is being weighed against this route. If yours is not here, send the drawing or specification and it is answered against the actual project.
The route is chosen from the part rather than from a preference for a process. The casting size and the tightest feature on the drawing decide whether a heated metal pattern earns its place, because the bonded shell is a route for small and medium castings rather than heavy ones. Where the drawing needs more than this route can hold, the step up is reviewed against investment casting. Whether the volume justifies a metal pattern belongs to the same review, and a complete-line scope is defined only after the casting, material and production requirement are agreed.
It depends on what the tooling was built for. The shell is formed against a heated pattern, so the pattern has to be a metal tool that takes repeated heating, and tooling built for a room-temperature route may not suit it. A pattern can sometimes be adapted to a different machine or plate, and coreboxes are often easier to adapt than pattern plates. What is possible is confirmed against the drawing, the material and the project, together with the condition and the records of the existing tooling.
The wall is set on the heated pattern, mainly by how long the resin-coated sand stays in contact with the hot surface before the loose sand is drained away. The cure is then finished with heat so the bonded layer reaches the strength the pour will demand. Wall and cure are chosen for the casting being made rather than from a fixed value, because a shell that is too thin and a shell that is too thick fail in different ways. Both are confirmed against the drawing, the material and the project.
Cores are optional and are added only when the casting needs an internal passage or a hollow area that the shell cavity cannot form. They are produced on the same hot box principle, on a heated corebox with resin-coated sand, and their shape follows the internal feature on the drawing. Cores are set into the cavity before the shell is closed, so core design and shell design are reviewed together. Whether a core is needed, and how it is supported, is confirmed against the drawing, the material and the project.
The two halves are brought together with a core already in place where one is needed, and they are held by the closing method chosen for the design, which may be an adhesive, a clamp or both. The closed shell then moves to the casting line and is backed for the pour, because the bonded layer is thin and the metallostatic pressure acts on it. How the halves are joined and how the mold is backed follow the mold design and the pouring route, and both are confirmed against the drawing, the material and the project.
The sand that does not bond to the shell is drained away and returned for the next cycle, so coated sand is handled as a circulating material rather than a single-use one. The coated sand keeps when it is stored cool and dry, because heat, moisture and pressure are what make it lump. Its condition is checked before use, and a batch that has taken up moisture or set into lumps is not run as if it were fresh. Storage and return are confirmed against the material and the project rather than assumed from the grade.
No. A smoother as-cast surface and a tighter as-cast tolerance do not reduce the stock that a machined face still carries. Machining allowance is set by the drawing and by the face being machined, and this route does not change the allowance such a face requires compared with other sand routes. Whether a face can be left as cast, or has to be machined, is a drawing and design question, confirmed against the drawing, the material and the project rather than assumed from the finish.
It starts from the process stage that formed the feature, not from the defect name. The investigation frame on this page groups the characteristic faults of the route with the stage each one is usually traced back to, so the review moves through shell condition, the stage that produced it, and the pouring and cooling steps in order. A single cause is not assumed, because faults in this route often come from more than one stage at once. The starting point is confirmed against the drawing, the material and the project.
START A PROJECT
Share the casting type, material, geometry, current process or equipment question. The first discussion can focus on process fit before any complete-line scope is defined.